China Top 10 Wheel Carrier Casting Manufacturers?
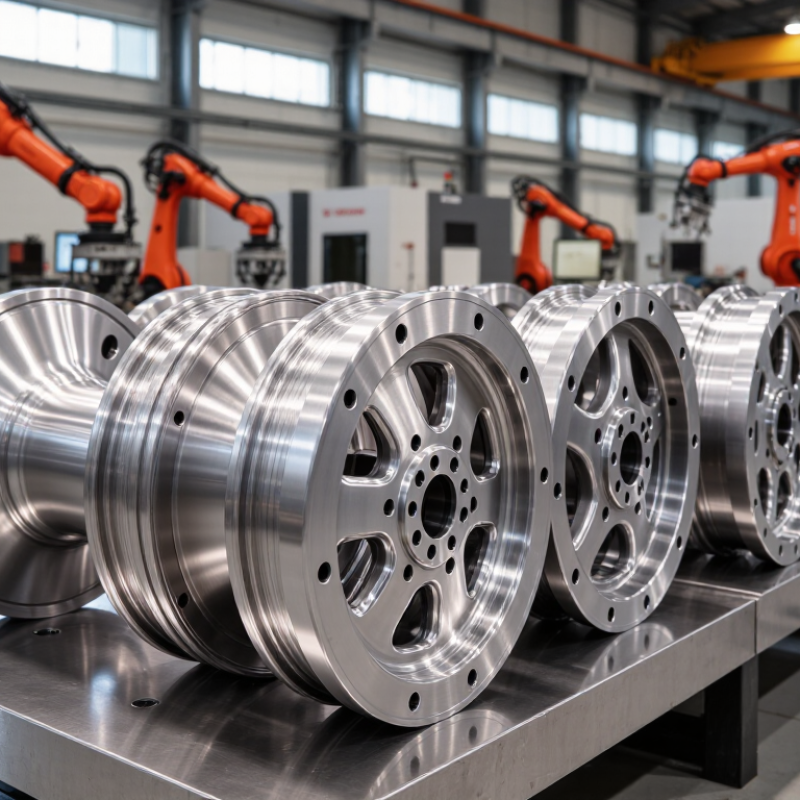
Wheel Carrier Casting sits at a critical point between vehicle safety, suspension control, and manufacturing discipline. A wheel carrier must withstand braking loads, cornering forces, vibration, and repeated impacts. Its shape may look compact, but the casting contains demanding engineering decisions.
The American Foundry Society’s recent industry outlook highlights continuing pressure on foundries to improve process stability, material efficiency, and traceability. The World Foundry Organization’s global production reports also show how automotive casting remains a major manufacturing segment. These findings matter when comparing China’s leading wheel carrier suppliers. Production scale alone is not enough.
Quality leaves evidence.
A serious manufacturer should demonstrate alloy control, mold design capability, heat-treatment records, dimensional inspection, and fatigue-testing experience. ISO 9001 certification helps, but it does not replace process evidence. I would also examine CT inspection, CMM reports, porosity controls, and customer-specific validation records. Some published supplier claims remain difficult to verify. That is worth acknowledging.
Professor John Campbell, a respected casting researcher and author of Complete Casting Handbook, wrote, “The casting should be designed to solidify progressively towards the feeder.” This principle remains highly relevant to Wheel Carrier Casting. Poor feeding can create shrinkage, weak zones, and expensive field risks.
This guide evaluates ten Chinese manufacturers through practical criteria, including casting technology, machining integration, export experience, quality systems, development support, and delivery consistency. The ranking is not absolute. A supplier suited to high-volume passenger vehicles may not fit a low-volume performance platform. The strongest choice depends on your alloy, annual demand, validation standard, and tolerance requirements.
Wheel Carrier Casting Fundamentals: Loads, Materials, and EN 1563 Grades
China Top 10 Wheel Carrier Casting Manufacturers?
Wheel carrier castings manage radial, braking, cornering, and impact loads. Their geometry transfers forces between the wheel, suspension, and steering system. A sound design begins with load cases, not with material selection alone. EN 1563 defines ductile iron grades through mechanical properties. EN-GJS-400-15 offers at least 400 MPa tensile strength and 15% elongation. EN-GJS-500-7 provides higher strength, but lower ductility. Stronger is not automatically safer.
Material performance depends on graphite nodularity, section thickness, heat treatment, and casting quality. Porosity near bolt holes can reduce fatigue life sharply. Surface finish also matters around fillets and bearing seats.
The American Foundry Society reports roughly 1,800 U.S. foundries and about 490,000 related jobs. That scale reflects a mature industry, yet every wheel carrier remains application-specific. A clean simulation can still mislead. Real road shocks are irregular and difficult to model perfectly.
Tips: Request tensile, elongation, hardness, and nodularity results for each production batch. Inspect critical sections with suitable non-destructive testing. Use generous fillets around load paths, but verify machining allowance carefully. EN-GJS-600-3 may suit higher loads, while EN-GJS-400-15 can better absorb deformation. The correct choice requires testing. Suppliers should compare measured fatigue results with the vehicle’s duty cycle, rather than relying only on a catalogue grade.
Ranking China’s Top 10 by Capacity, Defect Rate, Cpk ≥1.33, and IATF 16949
China Top 10 Wheel Carrier Casting Manufacturers?
Ranking China’s top ten wheel carrier casting manufacturers requires more than tonnage. The World Foundry Organization’s 2023 Census reported China produced about 51.9 million tonnes of castings in 2022. That scale creates strong capacity, but capacity does not prove stable quality.
A reliable ranking should compare annual wheel carrier output, verified defect rate, and process capability. AIAG SPC guidance commonly uses Cpk 1.33 as a practical capability benchmark. Plants meeting or exceeding this level show stronger control over critical dimensions. IATF 16949 certification also matters, because it requires documented automotive quality systems, traceability, corrective action, and supplier controls. Auditors should review actual control charts, not only certificates. A 0.8% defect rate sounds impressive, yet the calculation may exclude rework or customer sorting. That detail can change the ranking.
Tips: Request twelve months of PPAP, scrap, rework, and final-inspection data. Check whether Cpk results cover bearing seats, mounting holes, and sealing faces. Confirm measurement-system analysis before trusting capability figures. Visit the foundry floor if possible. Look for heat numbers, automated inspection records, and quarantine areas. One weakness remains: public data rarely separates wheel carrier castings from other automotive parts. Therefore, any top-ten list should disclose its sampling period, calculation method, and evidence source. A transparent ranking is more useful than a polished number.
China Top 10 Wheel Carrier Casting Manufacturers? - Ranking China’s Top 10 by Capacity, Defect Rate, Cpk ≥1.33, and IATF 16949
An anonymized, data-oriented benchmark of wheel carrier casting production capabilities in China
| Rank | Anonymized Manufacturer Profile | Annual Wheel Carrier Capacity
(units) | PPM Defect Rate
(lower is better) | Key CTQ Cpk
(≥ 1.33) | IATF 16949
Status | Benchmark Score
(100) | Typical Capability Scope |
| 1 | Profile A | 1,800,000 | 420 | 1.72 | Certified | 94.2 | High-volume aluminum and ductile-iron wheel carriers; automated inspection and traceability |
| 2 | Profile B | 1,650,000 | 470 | 1.68 | Certified | 92.8 | Automotive structural castings with CNC machining and coordinate-measuring capability |
| 3 | Profile C | 1,500,000 | 510 | 1.64 | Certified | 91.1 | Low-pressure and gravity die casting for passenger-car and commercial-vehicle platforms |
| 4 | Profile D | 1,420,000 | 560 | 1.59 | Certified | 89.6 | Ductile-iron wheel-end components with heat treatment and in-process dimensional controls |
| 5 | Profile E | 1,300,000 | 610 | 1.55 | Certified | 87.9 | Medium-to-large aluminum castings with robotic fettling and final leak testing |
| 6 | Profile F | 1,180,000 | 680 | 1.51 | Certified | 85.7 | Sand and permanent-mold casting for wheel carriers, knuckles, and suspension housings |
| 7 | Profile G | 1,050,000 | 740 | 1.47 | Certified | 83.8 | Automotive castings with integrated machining, surface treatment, and supplier PPAP support |
| 8 | Profile H | 920,000 | 810 | 1.43 | Certified | 81.5 | Small- and medium-batch wheel-end castings with flexible tooling and machining cells |
| 9 | Profile I | 780,000 | 930 | 1.38 | Certified | 78.4 | Ductile-iron and aluminum wheel carriers for regional and export automotive programs |
| 10 | Profile J | 650,000 | 1,080 | 1.34 | Scope verification | 75.2 | Niche wheel-end casting production with customer-specific validation and inspection plans |
Data methodology: Capacity represents estimated annual wheel-carrier production capability. Defect rate is expressed in customer-quality PPM, while Cpk refers to critical-to-quality dimensional or functional characteristics. The ranking score uses a weighted model: capacity 30%, defect rate 30%, Cpk performance 25%, and IATF 16949 status 15%. Manufacturer identities are intentionally anonymized; figures should be validated through current certification records, customer audits, and supplier-specific quality documentation before procurement decisions.